Incoming material
Each EVA or TPE lot arrives with its grade certificate. We check shore hardness and sheet thickness before it goes to the press, and keep the lot number against the batch.
Shore hardness ±3, thickness ±0.1 mm
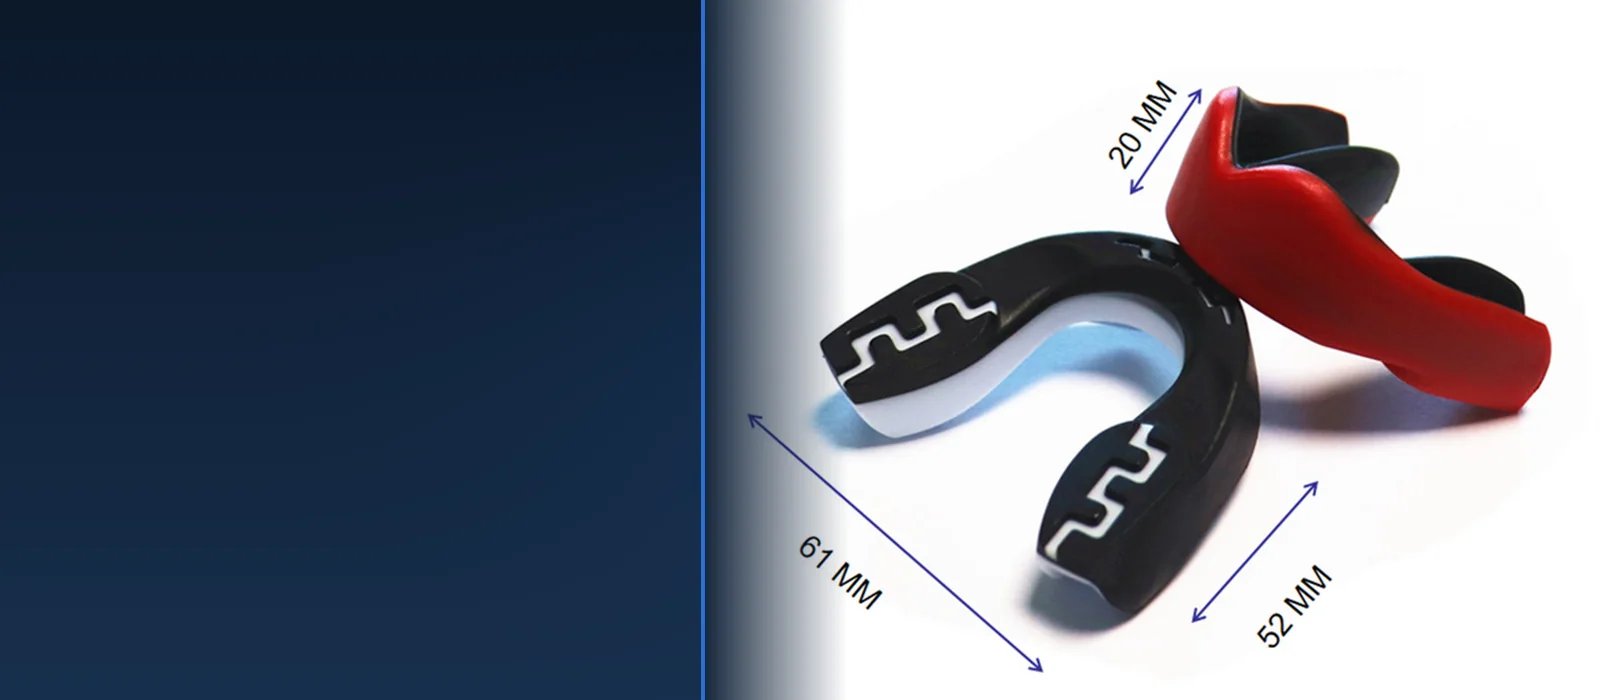
One plant in Dongguan: sheet comes in one door, printed guards in vented cases leave through the other. Six stages, four inspection gates, and the tooling kept upstairs so a reorder does not need a new sample round.
Output photos rather than machine photos: the presses, trimming benches and case line are what the live walkthrough below is for.
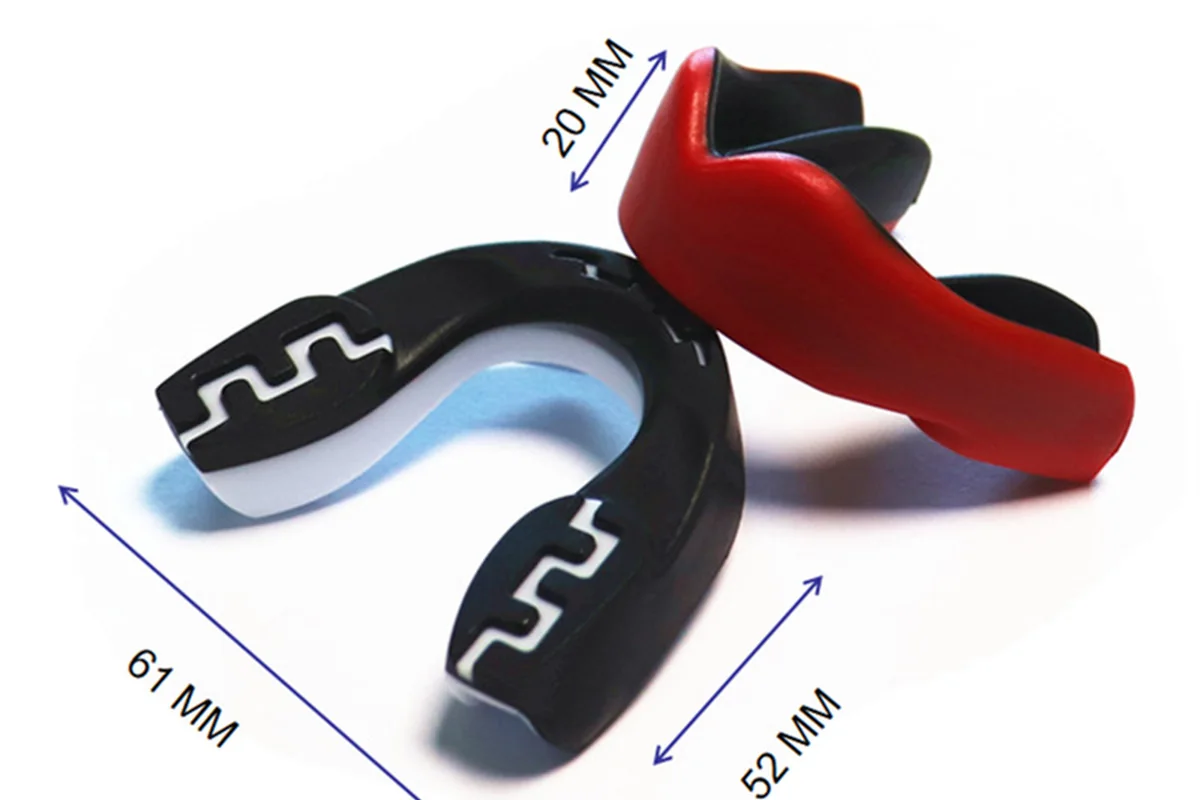
Wall thickness and arch dimensions marked — what gate 02 measures
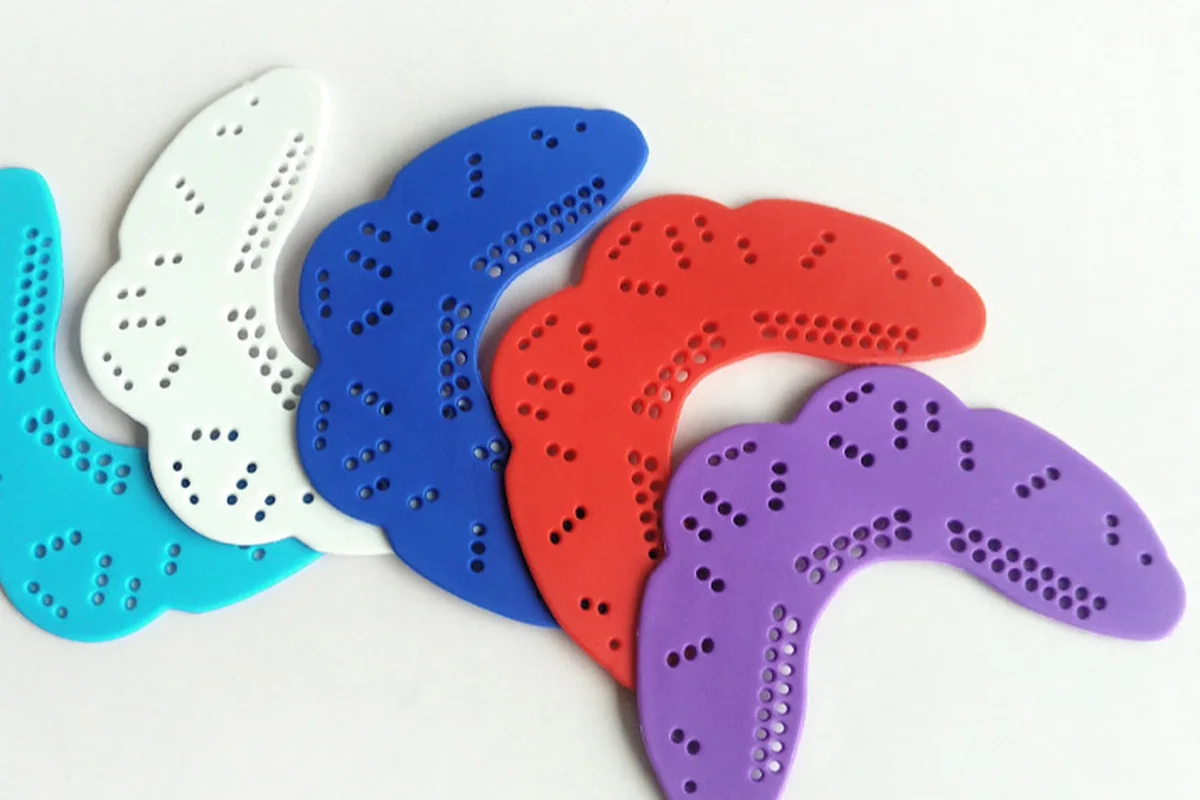
Printed shells laid out for inspection against the signed sample
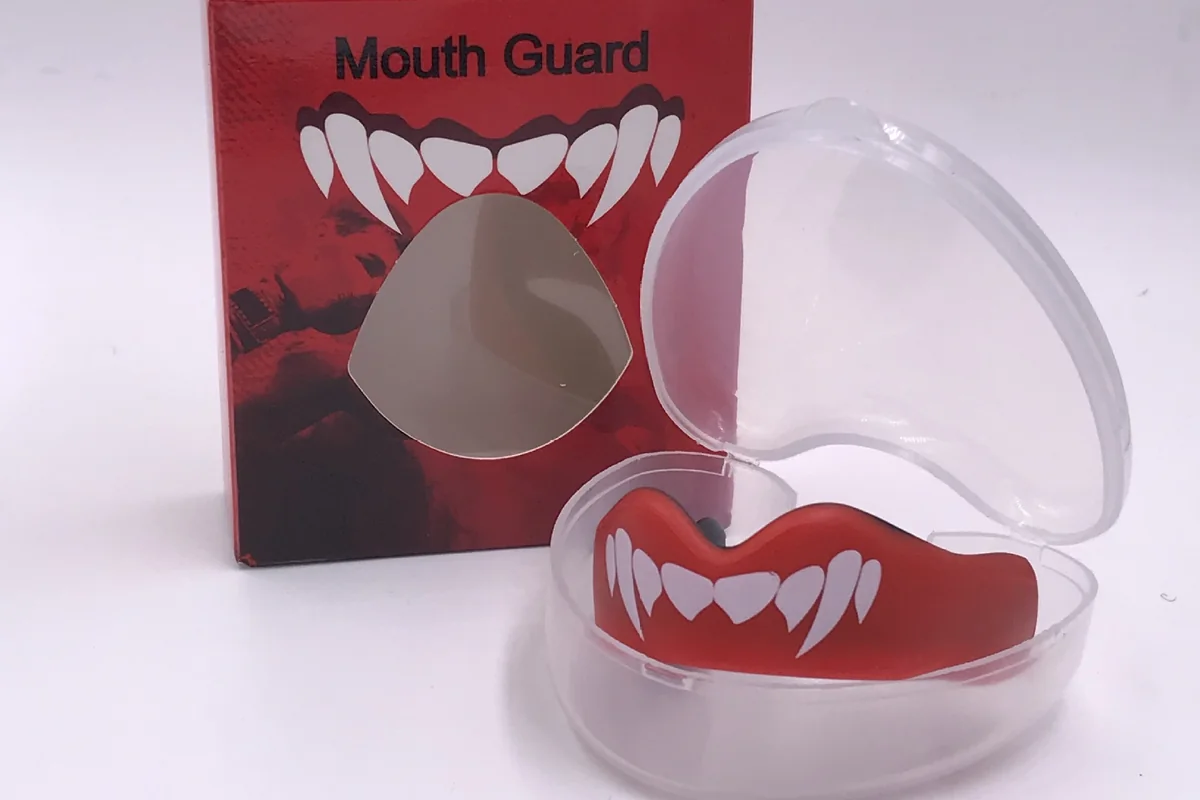
Retail pack: shell, vented case and printed box checked together
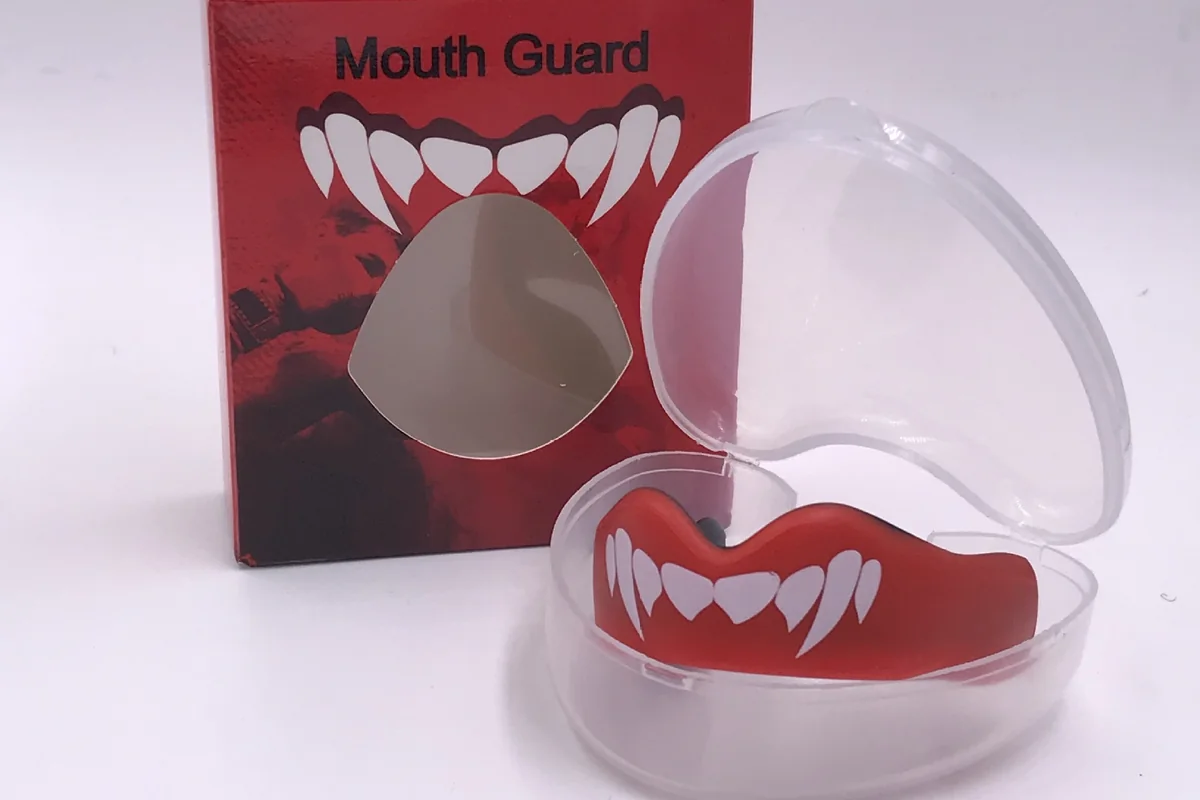
Cased set ready for carton packing, 200 sets per carton
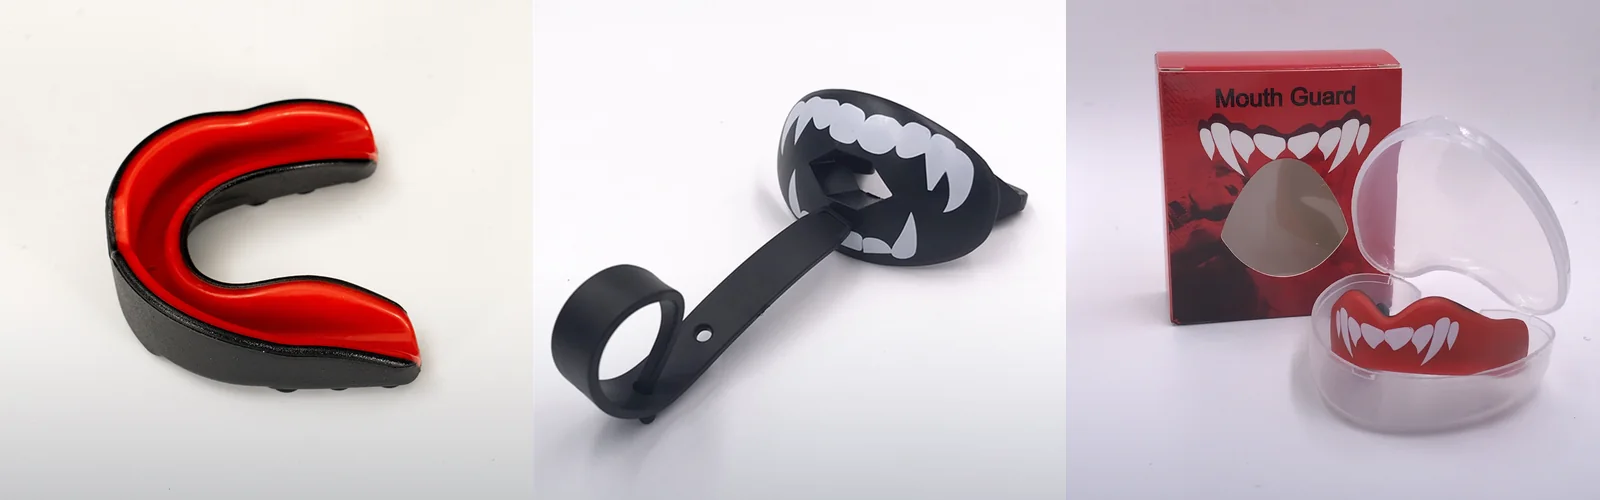
Three stages side by side: shell, tethered shell, cased set
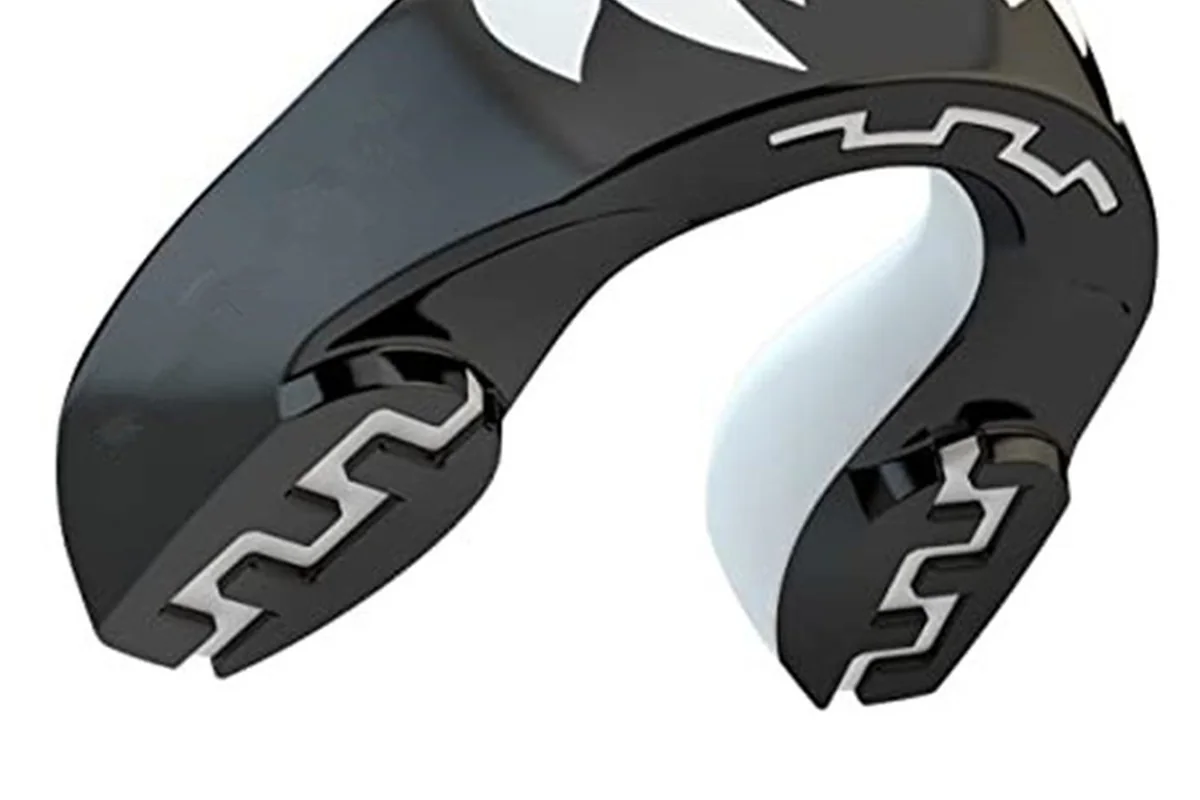
The signed sample kept on file for every reorder
Six process lines, 120+ people across three shifts, and a monthly ceiling of 300,000 pcs. A 100-piece trial and a 30,000-piece team programme run on the same tools and the same inspection sheet, which is why scaling up does not change the product.
Each gate has a number attached to it, because 'strict QC' is not something a buyer can check.
Each EVA or TPE lot arrives with its grade certificate. We check shore hardness and sheet thickness before it goes to the press, and keep the lot number against the batch.
Shore hardness ±3, thickness ±0.1 mm
Wall thickness is measured at the front, mid-arch and rear every 50 pieces. A shell outside tolerance is pulled and the press is reset before the batch continues.
Wall ±0.2 mm, every 50 pcs
Print registration is checked against the approved artwork, tether pull is tested on every batch, and the case hinge is opened and closed 20 times before packing.
Registration ±0.5 mm, tether 50 N
AQL 2.5 on the finished carton: shell, edge finish, colour against the signed sample, print, case and packing list. A photo report goes out before the carton is sealed.
AQL 2.5, photo report before shipping
Rather than a cut-together clip, we walk your line live on a video call: the press your shell runs on, the trimming bench, the print plate and the carton closing. It takes about fifteen minutes and you can ask the operator to measure a wall thickness while you watch.
A 15-minute video call, your shell on our press, and the inspection sheet in front of you.